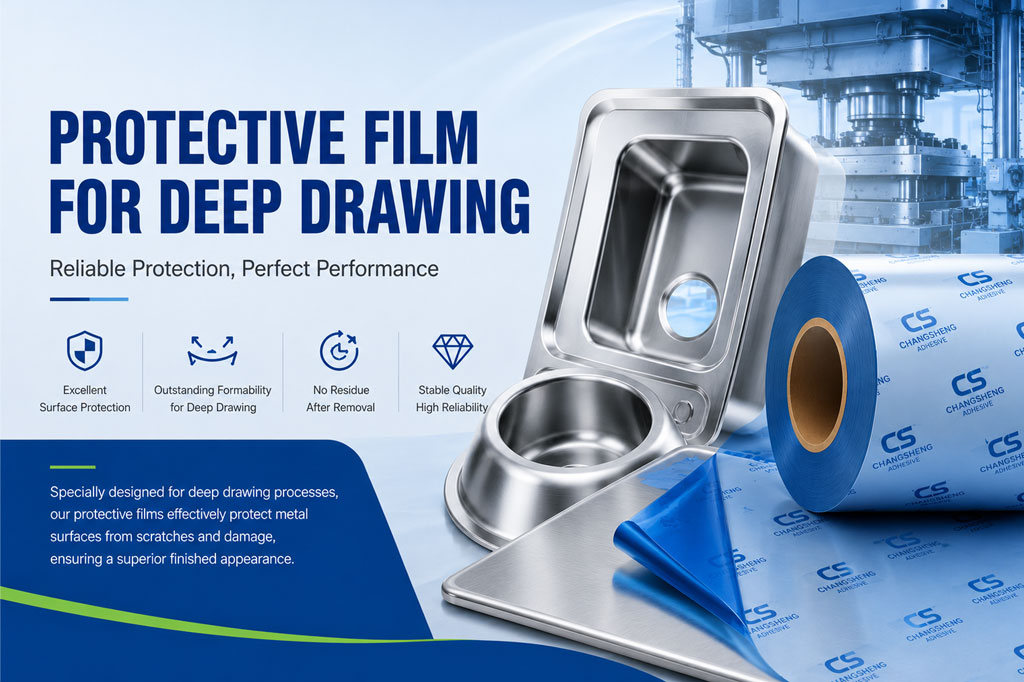
Deep drawing transforms a flat sheet of metal into a three-dimensional component by forcing it into a die. During this process, the metal—and any protective film applied to it—must stretch, bend and slide under considerable pressure.
A protective film that performs well during transportation or ordinary cutting may fail during forming. It can split at tight corners, lift from the surface, wrinkle after leaving the die or become difficult to remove.
Selecting the right protective film for deep drawing therefore requires more than choosing a film thickness and adhesion level. Three mechanical properties are especially important:
- Elongation
- Tear resistance
- Memory effect
These properties must work together with the adhesive system to keep the surface protected throughout forming and subsequent processing.
Why Deep Drawing Is Particularly Demanding
In a deep drawing operation, a punch pushes sheet metal into a die cavity while the material flows around the die radius. Different areas of the sheet experience different levels of tension, compression and friction.
Typical deep-drawn products include:
- Stainless steel sinks
- Refrigerator and dishwasher components
- Kitchen hobs and extractor fan parts
- Automotive panels and housings
- Aluminum enclosures
- Industrial containers
- Decorative metal components
The protective film is exposed to the same changing geometry as the metal. It must remain continuous as the sheet stretches and must maintain contact with the surface as the finished shape forms.
Common film failures include:
- Splitting at corners
- Tearing along the formed edge
- Excessive thinning
- Wrinkling or creasing
- Lifting from recessed areas
- Adhesive residue
- Surface marks caused by particles or coating irregularities
The severity of these risks depends on the drawing depth, tool radius, metal type, forming speed and number of processing stages.
1. Elongation: Can the Film Follow the Metal?
Elongation measures how far a film can stretch before it breaks. It is generally expressed as a percentage:
Elongation (%) = (Length after stretching − Original length) ÷ Original length × 100
A film with 300% elongation, for example, can theoretically extend to four times its original length before breaking under the specified test conditions.
However, this laboratory value does not tell the whole story.
Deep drawing creates multidirectional strain
Standard tensile testing usually stretches a film in one direction. During deep drawing, the film may be stretched simultaneously in several directions, particularly around corners and tight radii.
A suitable film therefore needs:
- Sufficient elongation in both machine and transverse directions
- Uniform deformation across its width
- Stable thickness during stretching
- Good conformability around complex shapes
- Consistent performance from batch to batch
What happens when elongation is too low?
Insufficient elongation can cause the film to:
- Crack at the beginning of the forming process
- Split at tight corners
- Bridge over recessed areas
- Expose sections of the metal surface
- Tear into small pieces that are difficult to remove
Can elongation be too high?
High elongation is valuable, but uncontrolled stretching can also cause problems. A film may become extremely thin in highly strained areas, reducing puncture and abrasion resistance.
The objective is controlled elongation—not simply the highest possible elongation value.
For most deep drawing applications, flexible PE protective film or another specially formulated polyolefin film is generally a better starting point than a rigid carrier film.
2. Tear Resistance: Stopping Damage From Spreading
Elongation and tear resistance are not interchangeable.
Elongation describes how far a film can stretch before breaking. Tear resistance describes how effectively it prevents an existing cut or defect from growing.
A film may have high elongation but still tear easily once a small defect has formed.
Where do tears usually begin?
Tears can start at:
- The edge of the metal blank
- A cut or nick in the film
- A sharp corner
- A gel or hard particle in the carrier film
- A non-uniform area in the adhesive coating
- A location where the film has become excessively thin
- A high-friction point between the sheet and tooling
Once the tear begins, the pressure and movement of the deep drawing process can rapidly propagate it across the film.
What should buyers evaluate?
A deep drawing protective film should have:
- High resistance to tear propagation
- Consistent tensile strength
- Good puncture resistance
- Uniform thickness
- Minimal gels and hard inclusions
- Resistance to drawing oils and moisture
- Adequate strength after stretching
Increasing film thickness may improve mechanical strength, but thickness alone cannot correct a poor resin formulation or non-uniform film structure.
3. Memory Effect: Will the Film Stay on the Formed Part?
Memory effect refers to the tendency of a stretched film to move back toward its original dimensions. It is also described as elastic recovery or restoring force.
After a component leaves the die, the stretched protective film may begin to contract. If the restoring force is too high, it can pull away from the newly formed geometry.
Excessive memory effect can cause:
- Edge lifting
- Wrinkles after forming
- Tunnels beneath the film
- Detachment around corners
- Loss of contact in recessed areas
- Peeling during subsequent production stages
This problem may not appear immediately. A component can look acceptable when it leaves the press but develop lifting or wrinkles several hours later.
Why low memory is important
A low-memory protective film remains conformable after deformation. It is particularly valuable when:
- The drawing depth is large
- The part has tight radii
- Forming takes place in several stages
- The film must remain on the component after pressing
- The formed part will be transported or assembled before film removal
Low memory does not mean that the film should have weak mechanical strength. It still needs sufficient cohesion to resist thinning and tearing. The correct film balances high elongation with controlled recovery.
Light vs Heavy Deep Drawing
Not every deep drawing process requires the same film construction.
| Requirement | Light deep drawing | Heavy deep drawing |
|---|---|---|
| Drawing depth | Low to moderate | Large |
| Tool radius | Relatively wide | Tight |
| Film deformation | Moderate | Severe |
| Typical carrier | Flexible PE | Modified PE or polyolefin |
| Main requirements | Balanced adhesion, elongation and clean removal | High elongation, tear resistance and low memory |
| Common risk | Local lifting or moderate tearing | Edge tearing, excessive thinning and film recovery |
| Processing stages | Often single-stage | May involve multiple stages |
| Protection period | Frequently removed after forming | May remain through later processing |
The boundary between light and heavy deep drawing cannot be determined by drawing depth alone. Part geometry, metal thickness, lubrication, forming speed and tool design also influence the actual strain placed on the film.
Common Problems and Corrective Actions
| Problem | Possible cause | Corrective action |
|---|---|---|
| Film splits at tight corners | Insufficient elongation | Use a more flexible PE or modified polyolefin carrier |
| A small cut spreads across the film | Low tear propagation resistance | Improve carrier formulation, thickness or edge quality |
| Film lifts several hours after forming | Excessive memory effect | Select a lower-restoring-force carrier |
| Film moves inside the die | Insufficient adhesion or surface contamination | Adjust adhesion and improve surface preparation |
| Wrinkles appear after pressing | Uneven stretching or high recovery force | Review film uniformity, lamination tension and memory |
| Adhesive residue remains | Cohesive failure, lubricant interaction or excessive dwell time | Test a more compatible PSA formulation |
| Marks appear on polished metal | Gels, particles or uneven coating | Improve film cleanliness and coating uniformity |
| Removal deforms the part | Excessive peel force | Reduce adhesion or use an application-specific easy-removal formulation |